Tuesday, December 29, 2009

Playing Tag

I’m about 95% finished with restoring the Kelton intaglio press. Later I’ll post more about the adventure of cleaning and adjusting it, which turned out to be a bigger job than I had at first suspected. This was mostly because after it left its useful life as a working press it lay somewhere getting rusty before the next owner applied black paint to every surface whether it was dirty, rusty, greasy, or was supposed to be painted or not. They then used it for a display piece which is also what the next owner intended for it when he got a lobby. Since this lobby never materialized, I now own the press. The net result is that many things were frozen and a lot of paint had to be removed which revealed a lot of rust that had to be removed. In the end it was fine but time consuming.

Anyway, I was so anxious to try something I had never done before, namely intaglio printing, and so much wanted to see whether or not the press actually worked that I threw caution to the winds. After final adjustments Sunday afternoon I had things just together enough to pull a proof. The problem was that I had virtually nothing that one needs to do this; nothing proper that is. I had no intaglio ink, copper plate, tarlatan rag, hot plate, or blotting paper. And I had only watched some Youtube videos and read about the process in a few vintage books I downloaded free online. But fools rush in where angels fear to tread.

I did have a few scraps of felt and some 100% cotton paper however. Also some rubber base letterpress ink and a couple 2” diameter brass key ID tags that had been stamped with numbers. Into one of these I made some scratches to try the drypoint technique. The end results can be seen below. Keep in mind that I didn’t wipe off the (wrong) ink properly and that punched numbers are not the same as etching or engraving; also that I wet the paper too much and didn’t blot it properly; and top all of that the fact that I was rushing a bit to get it done after a long day. They may be some of the worst intaglio prints ever but in the above context didn’t come out too badly for some quick test prints. I certainly got a thrill from the “accomplishment” and the knowledge that the press actually worked. If you look closely you can see my backwards initials in the little scratched box in the second photo. These lines are extremely fine and it surprised me how well they showed up.


I’ll detail in another post the last stages of the restoration and have some photos of the restored press as well as a few more things I learned about it.

Sunday, December 13, 2009

Sign Of The Time

The time in this case is somewhere in the latter half of the 19th century. I found a little time capsule in the Kelton copper plate press today. But let me lay some groundwork.

Presses of this type, especially older ones, needed the lower roller adjusted to come into contact with the underside of the press bed. This was done quite simply using shims under the bronze bearing blocks. Any hard, stable material will do, thick and thin pieces being used as required. Wood and paper were sometimes used but these materials are dynamic, expanding or contracting with changes in the humidity, and therefore not the best. A possible exception would be oiled paper such as tympan that is both hard and stable. Steel, iron, copper, and brass were all more appropriate choices.

I had disassembled the Kelton as much as possible with the exception of the lower roller. I was able to remove the bearing blocks and shims but removing the roller itself would require taking the main frame completely apart. This wasn’t necessary as I could clean everything with the roller in place and supported by two pipes. I cleaned the bearing blocks today and the shims and it was here that I made my discovery.

The press has been moved at least four times in its life including from the factory to its first owner. Adjustment of the roller would have taken place after that first move and I think I know enough about the subsequent life of the press to state that no one has likely changed this initial adjustment. The roller is very heavy and holds the shims in place quite securely. By the time I got it the shims were pretty much glued in place as well with the gunk of the ages and the paint one of the previous owners had sloped on to make it shiny looking. Further examination bore out that they were certainly very old.

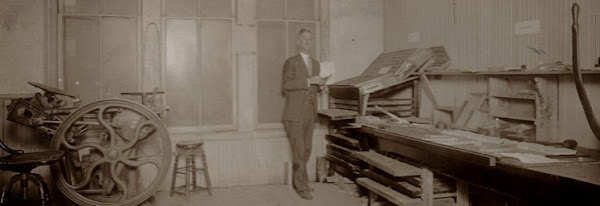
On both sides they consist of small steel plates, a few brass pieces of two different thicknesses, and on one side two pieces of oiled paper, possibly tympan. While the steel plates were for the most part unremarkable, one of them contained some evidence of the craft for which the press was intended. An example of this craft in action can be seen in the circa 1860 illustration below of the press room of the American Bank Note Company in New York City.


Copper and other plates used for intaglio printing have a bevel filed at the outer top edges, sometimes at a 45-degree angle but more often one less steep. The purpose of the bevel is to keep the otherwise sharp right angle of the edge from cutting into the paper under the great pressure exerted during printing. Anyone who has seen an intaglio print will likely remember that the edge of the plate is visible at the outside of the image. Even today plates do not come this way from the factory but the printer files the bevel himself. What I found on one of the steel shims was this hand-filed bevel.

The plate is 1/8” thick, a standard gauge for printing, and approximately 1 ¾” by 2” though not a perfect rectangle but a rather accurate parallelogram. As you can see from the photo, there are two holes drilled into it and it has numerous scratches in it. On one side the bevel is a fairly consistent 1/16” wide while on the reverse the edge has only been filed slightly, a distinct bevel but just enough to remove the sharp edge.


I can’t explain the reason why this small plate was prepared as if it was to be used for engraving or etching a print on it. Perhaps it was done for practice. Or perhaps when making a shim for the press the force of habit took over when removing the sharp burr at the edges. I do plan on reusing the original shims now that I’ve cleaned them and if further adjustments are needed simply adding to those. But I’m tempted to replace this one with a new piece of steel.

The stories this press could tell and in some ways is telling, eh?

Sunday, December 6, 2009

Look Out! Here Comes The Spider-Man.

If Peter Parker had wanted to be a print maker of a more ancient variety, he may very well have chosen intaglio as his medium. Had he done so he would have needed a copper plate press, sometimes called a spider-press because of its large spoked handwheel. I don’t spin webs of any size or catch thieves just like flies but I am in the process of restoring a vintage copper plate intaglio press. Eat your heart out, Spidey.

This press was built by the M. M. Kelton Company of Brooklyn, NY sometime from the 1850’s through the early 20th century. I haven’t been able to pin it down closer than that and have found little direct information on these presses. However, by doing a lot of internet research, piecing together tidbits of information including that gleaned form vintage photos and etchings, and disassembly and studying the press as part of its restoration, I’ve learned quite a bit. For one thing, this style of cast iron mass-produced press was used extensively by bank note companies as well as the U.S. Bureau of Engraving and Printing throughout the latter half of the 19th century. One of the largest users in my own area was the American Bank Note Company which had a printing house in Brooklyn, NY in addition to it’s headquarters in Manhattan. Brooklyn is of course where my press was made. Below is a photo of the ABNC’s now closed Brooklyn plant as it looks today.


Another photo shows these presses in operation and there are dozens, maybe hundreds of them churning out paper money, certificates, stamps, and all manner of financial documents. These presses were not designed for artists but for production. The top cylinder was in fact only a half-cylinder, its cross section appearing as a D-shape. The bed had a weight attached to the back that in conjunction with a pulley kept the bed in the forward position. When turning the handwheel an adjustable cam on the right side of the cylinder engaged with an adjustable mating cam on the bed which started the bed through the two (upper and lower) rollers automatically. Intaglio presses use three felt blankets laid over the paper and plate in order to cushion the pressure and press the paper into the incised plate to pick up the ink. On this press, the top blanket is attached to the top cylinder and a bar at the rear of the bed holds the other two blankets that extend along the bed under the upper cylinder.


Additionally, there is an iron frame above the press with a cross bar on which is a pulley. The blankets attached at the rear of the bed are held together at the front end where a rope is attached that goes over this pulley and on the end of which is a weight. When the press is at rest the bed is in its forward (start) position and the front end of the blankets are held up in the air out if the way so the plate and paper can be laid on the bed. Then the handwheel is turned, the bed is engaged and goes between the rollers making the print at which point it is automatically released merely by continuing to turn the handwheel. The bed automatically returns to its forward position and the blankets are automatically drawn up out of the way so the proof can be removed. Anyone who has operated an intaglio press will recognize the time saved with this arrangement. While not necessary for artist’s proofs, it’s a definite advantage for meeting production deadlines.


The press is not large but it is heavy. This is partly because the upper cylinder is solid, and even though the lower cylinder is a hollow casting it is very large and has thick walls as you would expect on an intaglio press because of the pressure exerted during printing. Modern presses have rollers about the same size top and bottom but it was common in the 19th century for the bottom roller to be much larger than the top as is the case here. Altogether the press weighs between 300 and 400 pounds, though that’s just an estimate. In practical terms it will print a plate up to 8” x 10”. The presses most recent use was as a display item in a print shop in Long Island City, i.e. Queens. It had been coated in black paint right over any dirt and rust so it would be nice and shiny. It needs to be completly cleaned and adjusted, the paint taken off where it shouldn't be, and some minor repairs made but otherwise nothing major. I suspect it came from the ABNC in Brooklyn when they closed that plant which is not too far away from its display post.


I have several letterpress printing projects that are a priority at the moment but I’ve begun the restoration process on this press and hope to be able to experiment within a month or so. I’ve never done intaglio before so it will be interesting. Besides limited edition proofs, I want to use it to produce artwork for my letterpress journal and also for artistamps that I can perforate on my Rosback perforator. I’ve seen some examples of work that is a combination of intaglio and letterpress so there are a lot of options, even if I don’t have radioactive blood.
Saturday, October 31, 2009

Good Vibrations

Many thanks go to David Lukens of the Lauchmen Printing Company in Lansdale, Pa. Dave very generously presented me with this paper jogger, a very nice 7” x 10” size perfect for most work. Dave has been a printer for years and years and is still hard at work doing what local print shops have always done: take care of his community’s basic printing needs. Schools, churches, businesses and individuals all make use of his skills and experience. While no longer doing letterpress work, he does all kinds of single and multi-color offset work (making his own plates), binding, folding, etc. His shop looks like a working print shop with cans of ink, paper of every description, boxes of envelopes, and all the misc. debris and brick-a-brac of printing laying about everywhere. While in some trades this is often considered a sign of sloppiness that is reflected in the work, such is most definitely not the case here. The work Dave produces is crisp and clean and he does this with easy efficiency. The old cry of “don’t clean it up or I won’t be able to find it” rings true here. The focus is on being productive and getting quality work out the door when customers want it and not maintaining a museum or laboratory environment. The proof is in the printing and Dave provides excellent work to happy customers.


A paper jogger is probably not one of the most needful things in a small shop, especially an amateur one like mine. But I do confess there have been times I’ve wished I had a way of more easily getting a nice even stack, especially when making pads. I happened to notice the wood table of the little jogger sticking out from among some debris on a bottom shelf while Dave was showing me around the shop and exclaimed, “Hey, what’s that under there?” Once pulled out it was obviously a jogger that Dave said he used to use but it hadn’t worked in a while. He then placed it in my hands and asked me if I wanted it.

Hmmm.

Once home I took it apart, cleaned it out, replaced the cracked and warped table, plugged it in and it was time to give it a workout. It was manufactured by the Syntron Company of Homer City, Pa. and is called the Syntron Paper Jogger, Type PJ4, Style 1763, Serial No. C8PJ65154. It has an on/off switch and a dial control to adjust the amount of vibration. The knob itself is missing and I’ll be picking up a replacement though it’s easy to adjust as it is. Based on the finish, construction and other little things I’m guessing the vintage to be 1930’s or 40’s. Syntron is now owned by FMC Technologies and is still making joggers today. I’m going to write to them to see if they can provide any information about mine from the serial number. But if anyone can narrow the date of my jogger down I’d appreciate it. Well, I’d write more but it’s time for my daily jog.

Sunday, October 25, 2009

Cinderella, She Seems So Easy; “It Takes One To Know One”, She Smiles.

Not too long ago I was reminded that not all stamps are postage stamps that pay for sending a letter from Point A to Point B. Some are in fact fantasy postage stamps, made up by someone to represent a fictional state, country, or protectorate. Some are made to advertise commercially or for non-profit organizations. Some promote various causes, groups, or anything at all. Some are simply ars gratia artis. In the worlds of art and craft they are commonly know as artistamps. Philatelically speaking such non-postage stamps are called Poster Stamps or Cinderellas.


The first postage stamps in the 19th century were printed in sheets and cut one singly with scissors or a knife. With the invention and marketing of the pin-hole perforator, separating them became much easier. Today postage stamps are self-adhesive and peel off a backer. But as I was reminded that not all stamps must comer from the Post Office and be used for postage, I was struck by the idea of letterpress printing my own stamps and perfing them. This is what I have in fact decided to do. I’ve done a bit of research and the consensus from those who do this kind of work with a printing press as opposed to an inkjet printer (which some do use) is that a cut should be made with anywhere from 4 to 12 images in the standard stamp sheet format. Here's a nice example from Rachel Scott at Fox Paw Press:

http://www.foxpawpress.com/Printshop/giftshop/artistamps/artistamps.html

All sorts of ideas come to mind and my first effort will be a simple Front Room Press stamp I can apply to envelopes or most anything. It will be a good opportunity to learn how to design something on the computer and have a plate made which I’ve never done. But even more fun will be to actually print and use them. This was a lot of my inspiration to get my perforator restored. Now it’s on to the next step. I’ll keep you posted.


Saturday, October 24, 2009

Holy Perforator!


The restoration of the perforator is complete and it actually works. Huzzah! Given the amount of rust and the condition of the punches it was no certain thing. For the most part cleaning was pretty straightforward if involved as described in my previous post. The punches and the holes they go in were the most tedious and troublesome part.


The perforator takes 365 punches about 1/32” diameter and 13/16” long. There are three parts that have holes for the punches: the punch holder, the stripper, and the die. So I had to clean out as best I could 1095 holes. I had soaked the parts repeatedly in WD40 after I finally got the punches out and after cleaning them completely I used one of the punches to scrape out the holes as much as possible. The last step here was pushing the punch through, wiping the WD40 off the far end, push it through again, wipe again, etc. until all of the extraneous WD40 was out. This actually worked pretty well and when I was done the punches all moved freely in the holes. The concern I really had was if they would go through freely when they had to pass through all three parts at once.

When these three parts were manufactured and the holes for the punches were bored they were clamped together in a jig and the holes bored through all three at the same time. The three parts were stamped with the same number so they could always be matched up. This is how alignment was always assured. Of course, a lot had happened to the perforator since it was new so it remained to be seen if this alignment remained.

I had picked up the replacement screws I needed and after the last one was replaced in the die I reassembled the stripper bar and its stiffener, reassembled the head, and then put the head back on the machine. I was almost done but looking at the punches I realized that I really needed to clean them down to bare, shiny metal and not leave them with any corrosion, no matter how minor. I was concerned about leaving them too long in the vinegar and salt bath because the surface of the metal becomes rough, if only mildly, and I wanted the smoothest surface possible to ease passage through the holes. What all this meant is that I would have to clean each punch one at a time. Fun, fun, fun.


Of the 365 punches the machine takes all had been present and I was able to recover 214 that were straight. There are perhaps 50 or so more that are only slightly bent and which I’m confident I can straighten out at some point and install. The complete row of punches is 24” long but even with only the 214 installed there are enough to perforate anything of a size I’m likely to need. I do plan on buying brand new punches in the near future because the ends on the old ones are not in the best shape and new punches will mean cleaner holes. But it punches good enough for any normal work, certainly not something the average person would notice.

Anyway, one by one using sandpaper I cleaned the punches, rolling them around with the tip of one finger on some chipboard while I sanded away with the other hand. I was careful not to sand in such a way to round over the edges on the working end of the punches but of course they weren’t perfect at this point anyway. This operation took episodes of Marcus Welby, Quincy, Kojak, Deal Or No Deal, the local news, two episodes of Judge Judy, Judge Joe Brown, and Ghost Whisperer to complete. Whew!

I installed the punches from the center of the head out so the pressure of the punching action would be centered. They went in better than I expected, with a few needing a slight helping hand from the tip of a screwdriver instead of my finger. I put oil on top of the stripper where the punches passed through and then started pumping the pedal. This was to break up remaining “stuff” in the holes and to lubricate things. I put some paper towels in harm’s way and stair-stepped my way to a cleaner, well-oiled perforator. I moved the paper towel with each step and it soaked up the excess “stuff” pretty well. It still leaves a slight residue on the top sheet but there is less each time and it works nice and smooth.

I had taken the tables to work to sand them with a pneumatic random orbit sander. This makes the work go fast and does a great job. The wood is cherry and was originally stained. Even though the tops of both tables had virtually no finish left it was intact on the underside and I found a match for it among some old cans of stain I had. I sanded enough to get rid of the dirt and paper that had been stuck to the wood when it had gotten wet, and to make everything smooth, but not enough to remove the patina. I stained it at home and then applied two coats of orange (amber) shellac, a traditional vintage topcoat. In the end I was surprised that the match was so close. I wasn’t worried about dents, bumps, chips, etc. because these tables have little affect on registration which is accomplished by the fences. Mostly the simply support the sheets.


Next time I’ll explain more about what I plan on doing with it besides the obvious, i.e. making holes. One thing I did realize is that because the holes are so small, this is a nice vintage option for general jobs requiring perfing instead of the more usual slit perf. The paper stays together well but tears very easily. And it won’t tear up the press rollers. Oh, boy!

Sunday, October 18, 2009

Stamp Act

I’m in the process of restoring a Rosback treadle-operated round-hole perforator circa 1920. It is 300 pounds of mostly cast iron with a 24” row of hundreds of tiny punches. Philatelically speaking it punches a perforation measurement of 12 which is, or rather was, the standard for U.S. stamps before 1914. Guess what I’ll be printing in the not too distant future? But more on that later.


While in generally good if typically dirty condition, the perforator had one serious problem: at one time it sat someplace where water was allowed to get onto the punch assembly. This assembly consists of three main parts besides said punches: the punch holder, the stripper, and the die. The punches are 13/16” long and a little over 1/32" diameter with a small head on one end like a brad. They drop into holes in the punch holder and down through the stripper bar. When the treadle is depressed the punches are pushed down through the stripper bar and into the die which has corresponding holes. Well, when stored at some point the head which carries the punch assembly was adjusted in such a way that the punches were pushed down below the bottom of the stripper. Add water, time, and neglect and presto! Rusted punches, punch carrier, stripper, and die plate. O joy!


Adding a bit to the sorrow is the fact that at some point someone with more physicality than patience tried to loosen the head and get the punches moving. To do this he inserted some kind of crow bar into the assembly and did what one does with a crow bar. While not loosening the punches it did have the affect of snapping the heads off four of the six screws by which the punch holder is attached to the head. His work apparently done, the perforator was left to get older. On the bright side the tables, while needing refinishing, are in good shape and it has both of its original fences with attachments. Also, it is not rusty to the same degree on all the punches.

Having disassembled and restored any number of antique machines in various degrees of decrepitude, I was reasonably certain that I could get it apart and that it could be cleaned and restored to use. The first step was to somehow get the punch assembly off the head and disassemble it. There was little point in cleaning anything else unless this could be accomplished. I sprayed on a liberal dose of PB Blaster “penetrating catalyst” and let it soak. I was prepared for a long process and this was the first step. Over the next three days I kept adding more Blaster and gently pried and tapped. No crow bar. During that time I was able to remove enough of the punches from both ends to get at the two bolts that hold the stripper bar to the bed. The stripper bar is attached to the bed and normally you can remove the entire head with the punches with the stripper bar remaining behind. But of course the punches were rusted to the bar. So in this case when I was finally able to lift off the head the stripper bar came with it.

Now I had access to the bottom of the stripper bar and after a couple more days of soaking I was able to tap the bottom of some of the punches to loosen them and pull them out. Just like pulling teeth, both descriptively and in terms of it being somewhat difficult. Keep in mind that there are literally hundreds of punches. I haven’t counted all of them yet but have got as far as 238. I got enough out finally to bend the stripper bar slightly and come at the screw heads of the last two screws holding the punch holder to the cast iron head using a right-angle screwdriver. More soaking and more tapping. It took a week but finally the last punch came out. Now all the parts needed to be cleaned down to original paint or bare metal. I don't like repainting unless absolutely necessary but I hate rust. I let the punches and some other parts soak overnight in a solution of vinegar and salt to loosen the rust up. Except for heavy rust this allows you to virtually wipe if off. In the process of removing the punches a number of them were bent or broken but I saved about 230 and I’m hoping they will work once clean. Replacements seem to be available from a couple sources and I’ve been in touch to get particulars. If the price is right I’ll replace them all and keep the old ones as spares.

Four screw heads had been broken off in the head and I had to drill out the remaining parts of the screw. I’ll pick up replacements at the hardware store. Cleaning itself was straight forward using WD-40; sandpaper; 3M green pads; a wire brush on a grinder and drill; and lots of paper towels. I’m not afraid to use sandpaper to get heavy rust off, stopping as soon as I get to bare metal. Then it’s the green pads and finally the wire wheel to make it nice. I used one of the old punches to clean out the inside of the hundreds of holes in the punch holder, stripper bar, and die plate. They weren’t that bad, the punches having provided some protection from direct exposure. But this part of the job was very tedious and cleaning the holes in the three parts took 5 hours. I did this in the evening while watching TV.

The main frame has been cleaned and the die plate reinstalled but for one screw that needs to be replaced. Once I get that screw and the others I need everything can be reassembled. At that point we’ll see if actually works. I hope to refinish the wood tables this week at work. More on that and what exactly I’ll be doing with it will wait for another post.